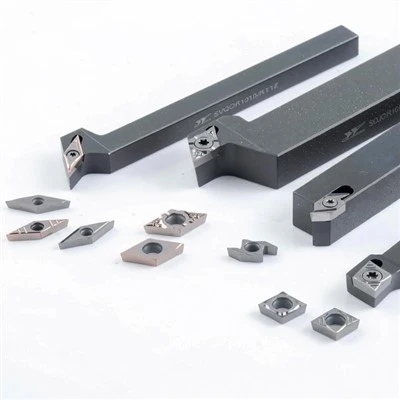

PCBN welded turning inserts with YP geometry are designed for precision turning of hardened and quenched steel. The specially designed BHF and BHM chip-breaker geometries help maintain stable chip control across different cutting depths, supporting consistent machining performance in finishing and precision-turning operations.
Key Features
Specialized YP chip-breaker geometry
Designed to support reliable chip breaking when turning hardened steel.
01
Two geometry options
BHF is suited to smaller cutting depths, while BHM is designed for larger cutting depths.
02
Stable machining performance
Helps improve chip management during continuous precision turning and selected intermittent operations.
03
For hardened steel applications
Suitable for demanding turning tasks involving quenched steel components.
04
Welded PCBN construction
A PCBN cutting edge is brazed onto the insert body for precision machining applications.
05
Geometry Selection
|
Geometry |
Recommended Cutting Depth |
Typical Use |
|
BHF |
0.1–0.3 mm |
Smaller cutting depths when turning hardened steel |
|
BHM |
0.3–0.8 mm |
Larger cutting depths when turning hardened steel |
Applications
These PCBN welded turning inserts are intended for precision machining of hardened steel parts, including tooling and mould-related components. Depending on the component design and machining setup, applications may include internal or bore turning, continuous precision turning, and selected intermittent face-turning operations.
Example Cutting Data
The following values are an example from a hardened-steel machining case. Actual cutting conditions should be adjusted according to workpiece hardness, tool overhang, machine rigidity, workholding, and the required surface finish.
|
Insert specification |
DNGG150408L-BHF |
|
PCBN grade |
BHC210P |
|
Workpiece material |
H13 tool steel, 52 HRC |
|
Cutting speed (Vc) |
200 m/min |
|
Feed rate (f) |
0.1 mm/rev |
|
Depth of cut (ap) |
0.25 mm |
|
Cooling method |
Dry cutting |
|
Machining operations |
Internal/bore turning; continuous precision turning; intermittent precision face turning |
Why Choose YP Geometry PCBN Inserts?
Choosing the appropriate chip-breaker geometry is important when machining hardened steel. The BHF and BHM options provide different cutting-depth ranges, helping users select a geometry that better matches the machining allowance and operation. Correct insert selection and stable cutting conditions can contribute to controlled chips, consistent surface quality, and dependable production performance.
Selection Notes
Select BHF for a cutting depth of approximately 0.1–0.3 mm, or BHM for approximately 0.3–0.8 mm.
Confirm insert shape, size, nose radius, and toolholder compatibility before ordering.
Use the example cutting data as a starting reference, not as a universal setting.
For best results, verify the recommended PCBN grade and cutting parameters for the specific workpiece material and hardness.

Request a Quote
Please share your workpiece material, hardness, machining operation, insert specification, and target cutting conditions. Our team can help you identify a suitable PCBN turning insert configuration for your application.
Hot Tags: pcbn turning inserts, China pcbn turning inserts manufacturers, suppliers, factory, Indexable Milling Insert, iso metric threading inserts, laydown carbide threading inserts, thread turning carbide inserts, thread turning inserts for cnc lathes, threading inserts for titanium